Process
From filament to finished sling
Five stages, the same for every sling, whatever its size.
 01
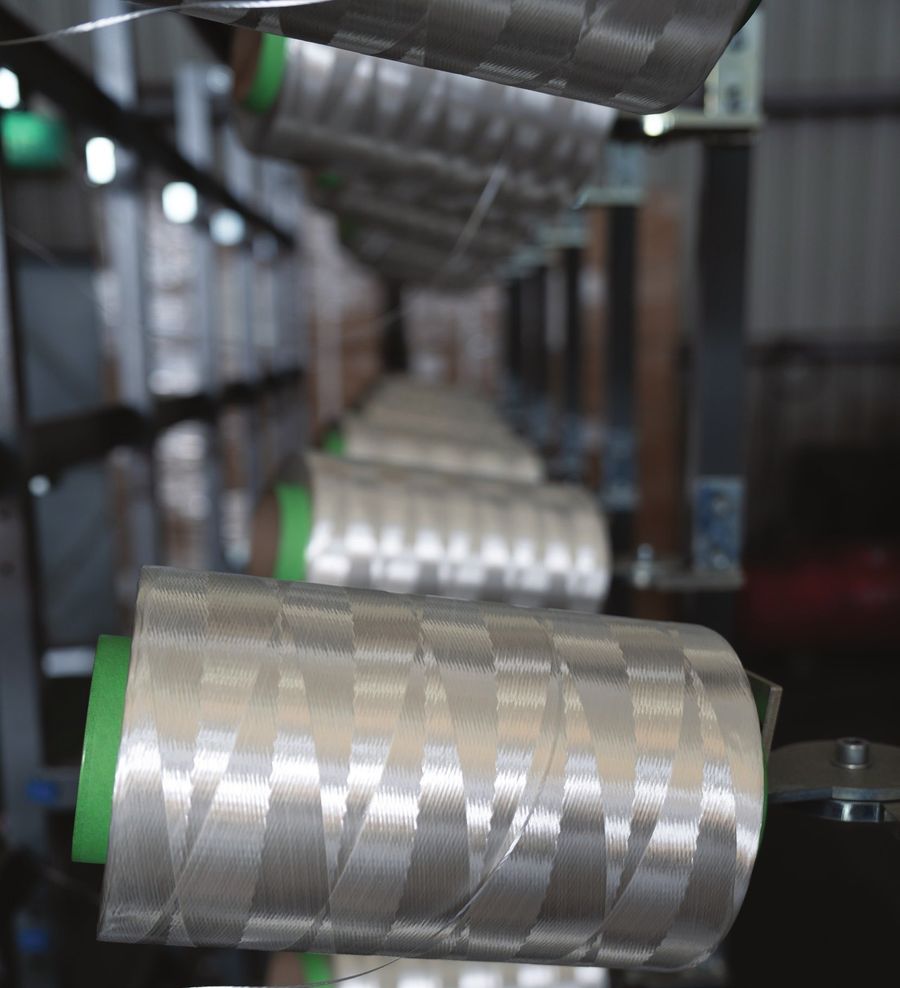
Filament · NX-98
UHMWPE filament from an audited, ESG-compliant supply chain, each lot checked against supplier certification before release.
 02
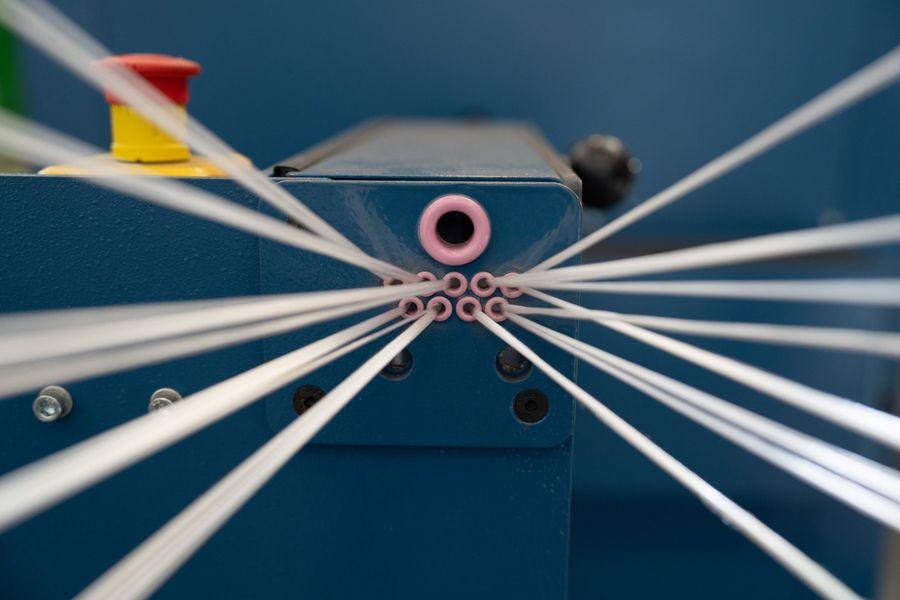
Yarn · NX-T110
Twisted in-house on best-in-class machinery and tested beyond industry practice. Superior twisted yarn engineered for strength and consistency.
 03
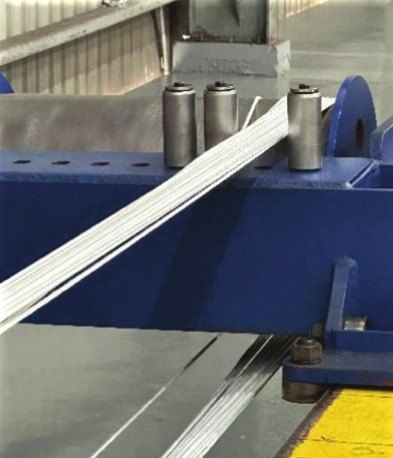
Core · parallel-laid hank
Yarn wound as a continuous parallel-laid hank under controlled, consistent tension: tight length tolerance and uniform elongation, so matched slings stay matched.
 04
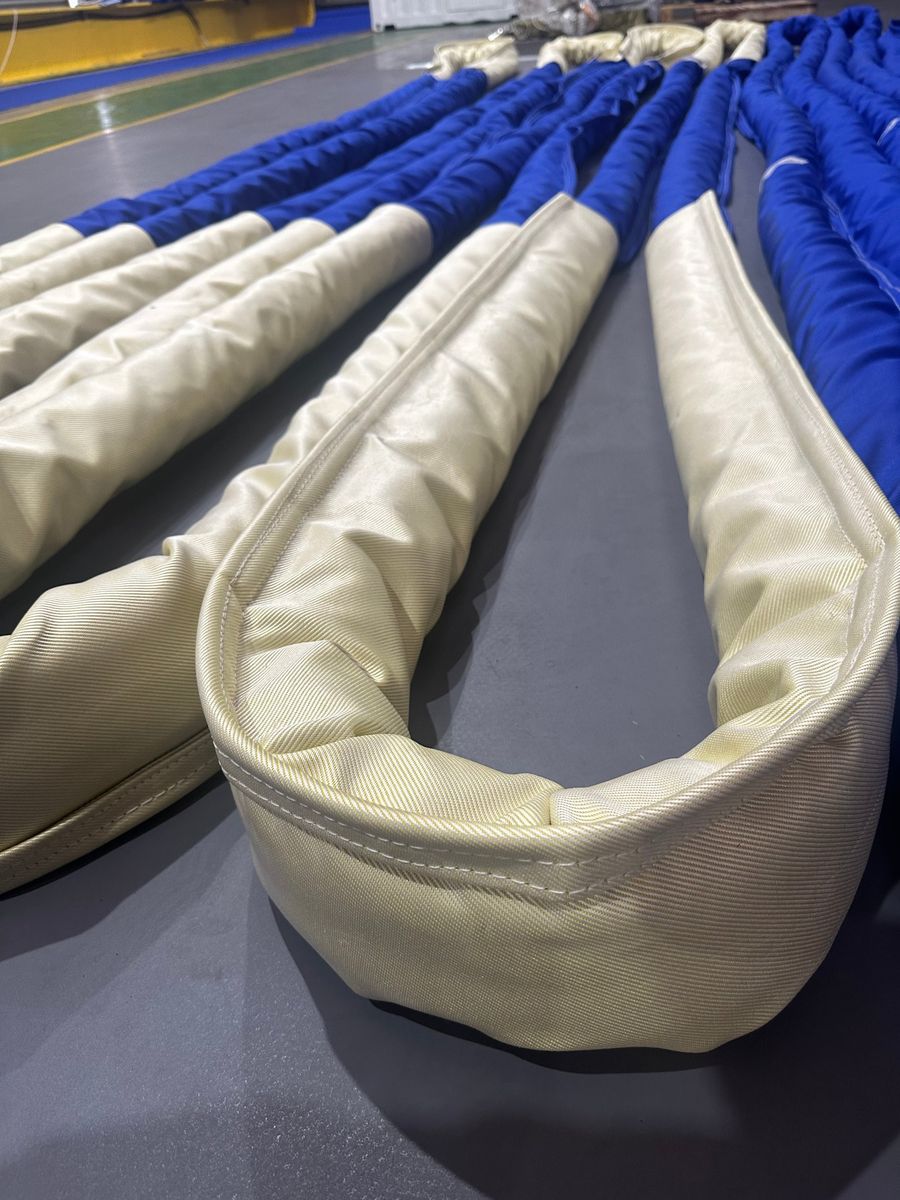
Cover · NEXOS & options
Double-bonded NEXOS (PES) body cover as standard, with NEXOS HD hybrid HMPE/PA at the bearing points. Full HMPE covers, sand filters and other options to suit the job.
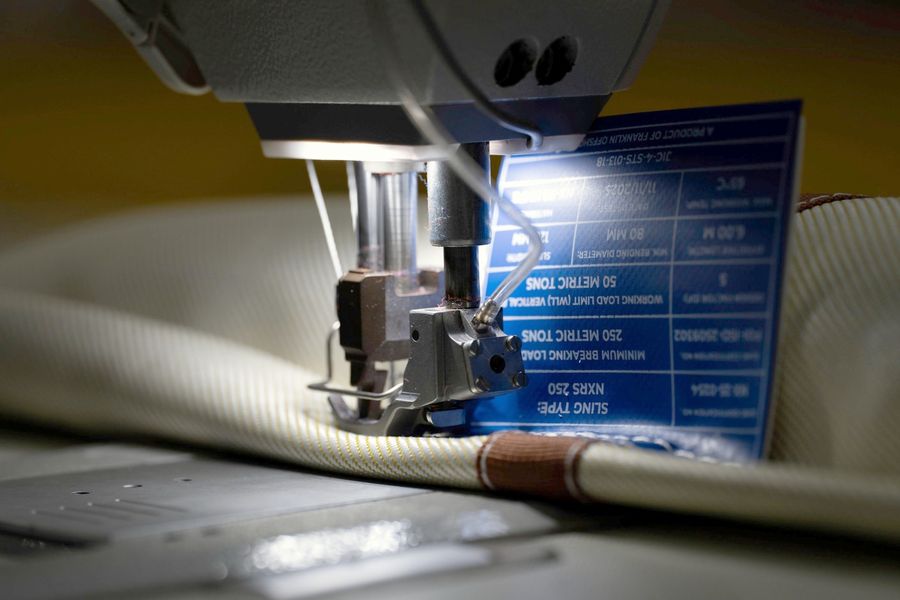 05
Sewing & identification
Structural lock stitching and hard-wearing ID tags carrying the sling’s full identification, sewn by trained NEXUS sewers, then on to 100% proof load testing.